IKV: Research for Practical ApplicationInnovations in TPS Foam, Lightweight Construction with UD Tapes, and Viscosity Control
A guest post by
Prof. Dr.-Ing. Christian Hopmann, Director of the IKV Institute and Chair of Plastics Processing; Viet-Anh Vu, M.Sc., Starch Foam Films; Tom-David Stüven, M.Sc., High-Performance Molded Parts; Katharina Baum, M.Sc., Viscosity Control
| Translated by AI
6 min Reading Time
Whether it’s flexible foam films made from starch, lightweight construction using UD tapes, or AI-based viscosity control for recycled materials—IKV Aachen is charting new paths for practical applications. How can sensitive biopolymers be processed reliably? What cost-saving potential do bionic reinforcing inserts offer? And how can viscosity be balanced during the ongoing compounding process?
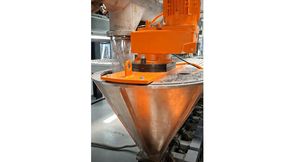
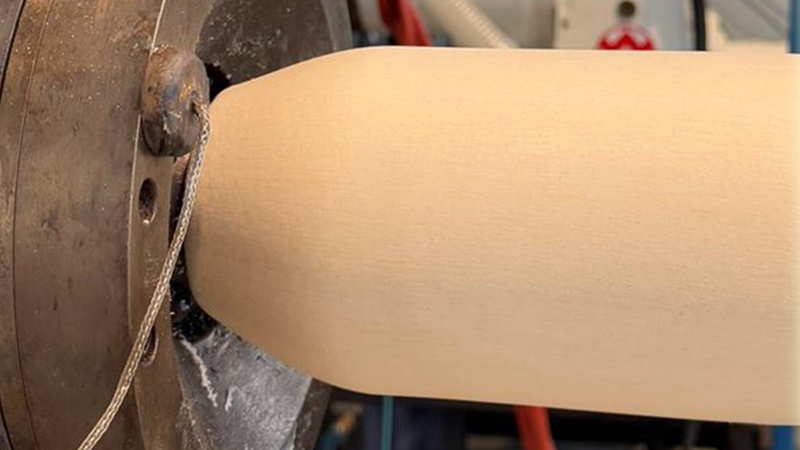
Using thermoplastic starch as a base, researchers at the IKV successfully produced a flexible foam film using physical blowing agents.
(Bild: IKV)
Foam Extrusion of Starch-Based Thermal Paste
Industrial foam films, such as those used for packaging or impact sound insulation, consist primarily of polymers derived from fossil-based raw materials, which are often thermally recycled after a single use. One way to make extruded foam products more sustainable is to use renewable raw materials, such as starch. However, the production of flexible foam films from thermoplastic starch (TPS) has been virtually impossible to date due to TPS’s low melt strength and narrow processing window. To expand the process window for the production of low-density flexible starch foam films, researchers at the IKV, as part of a project funded by the Federal Ministry of Food, Agriculture, and Home Affairs (BMELH), investigated the use of blowing agent mixtures based on CO2.
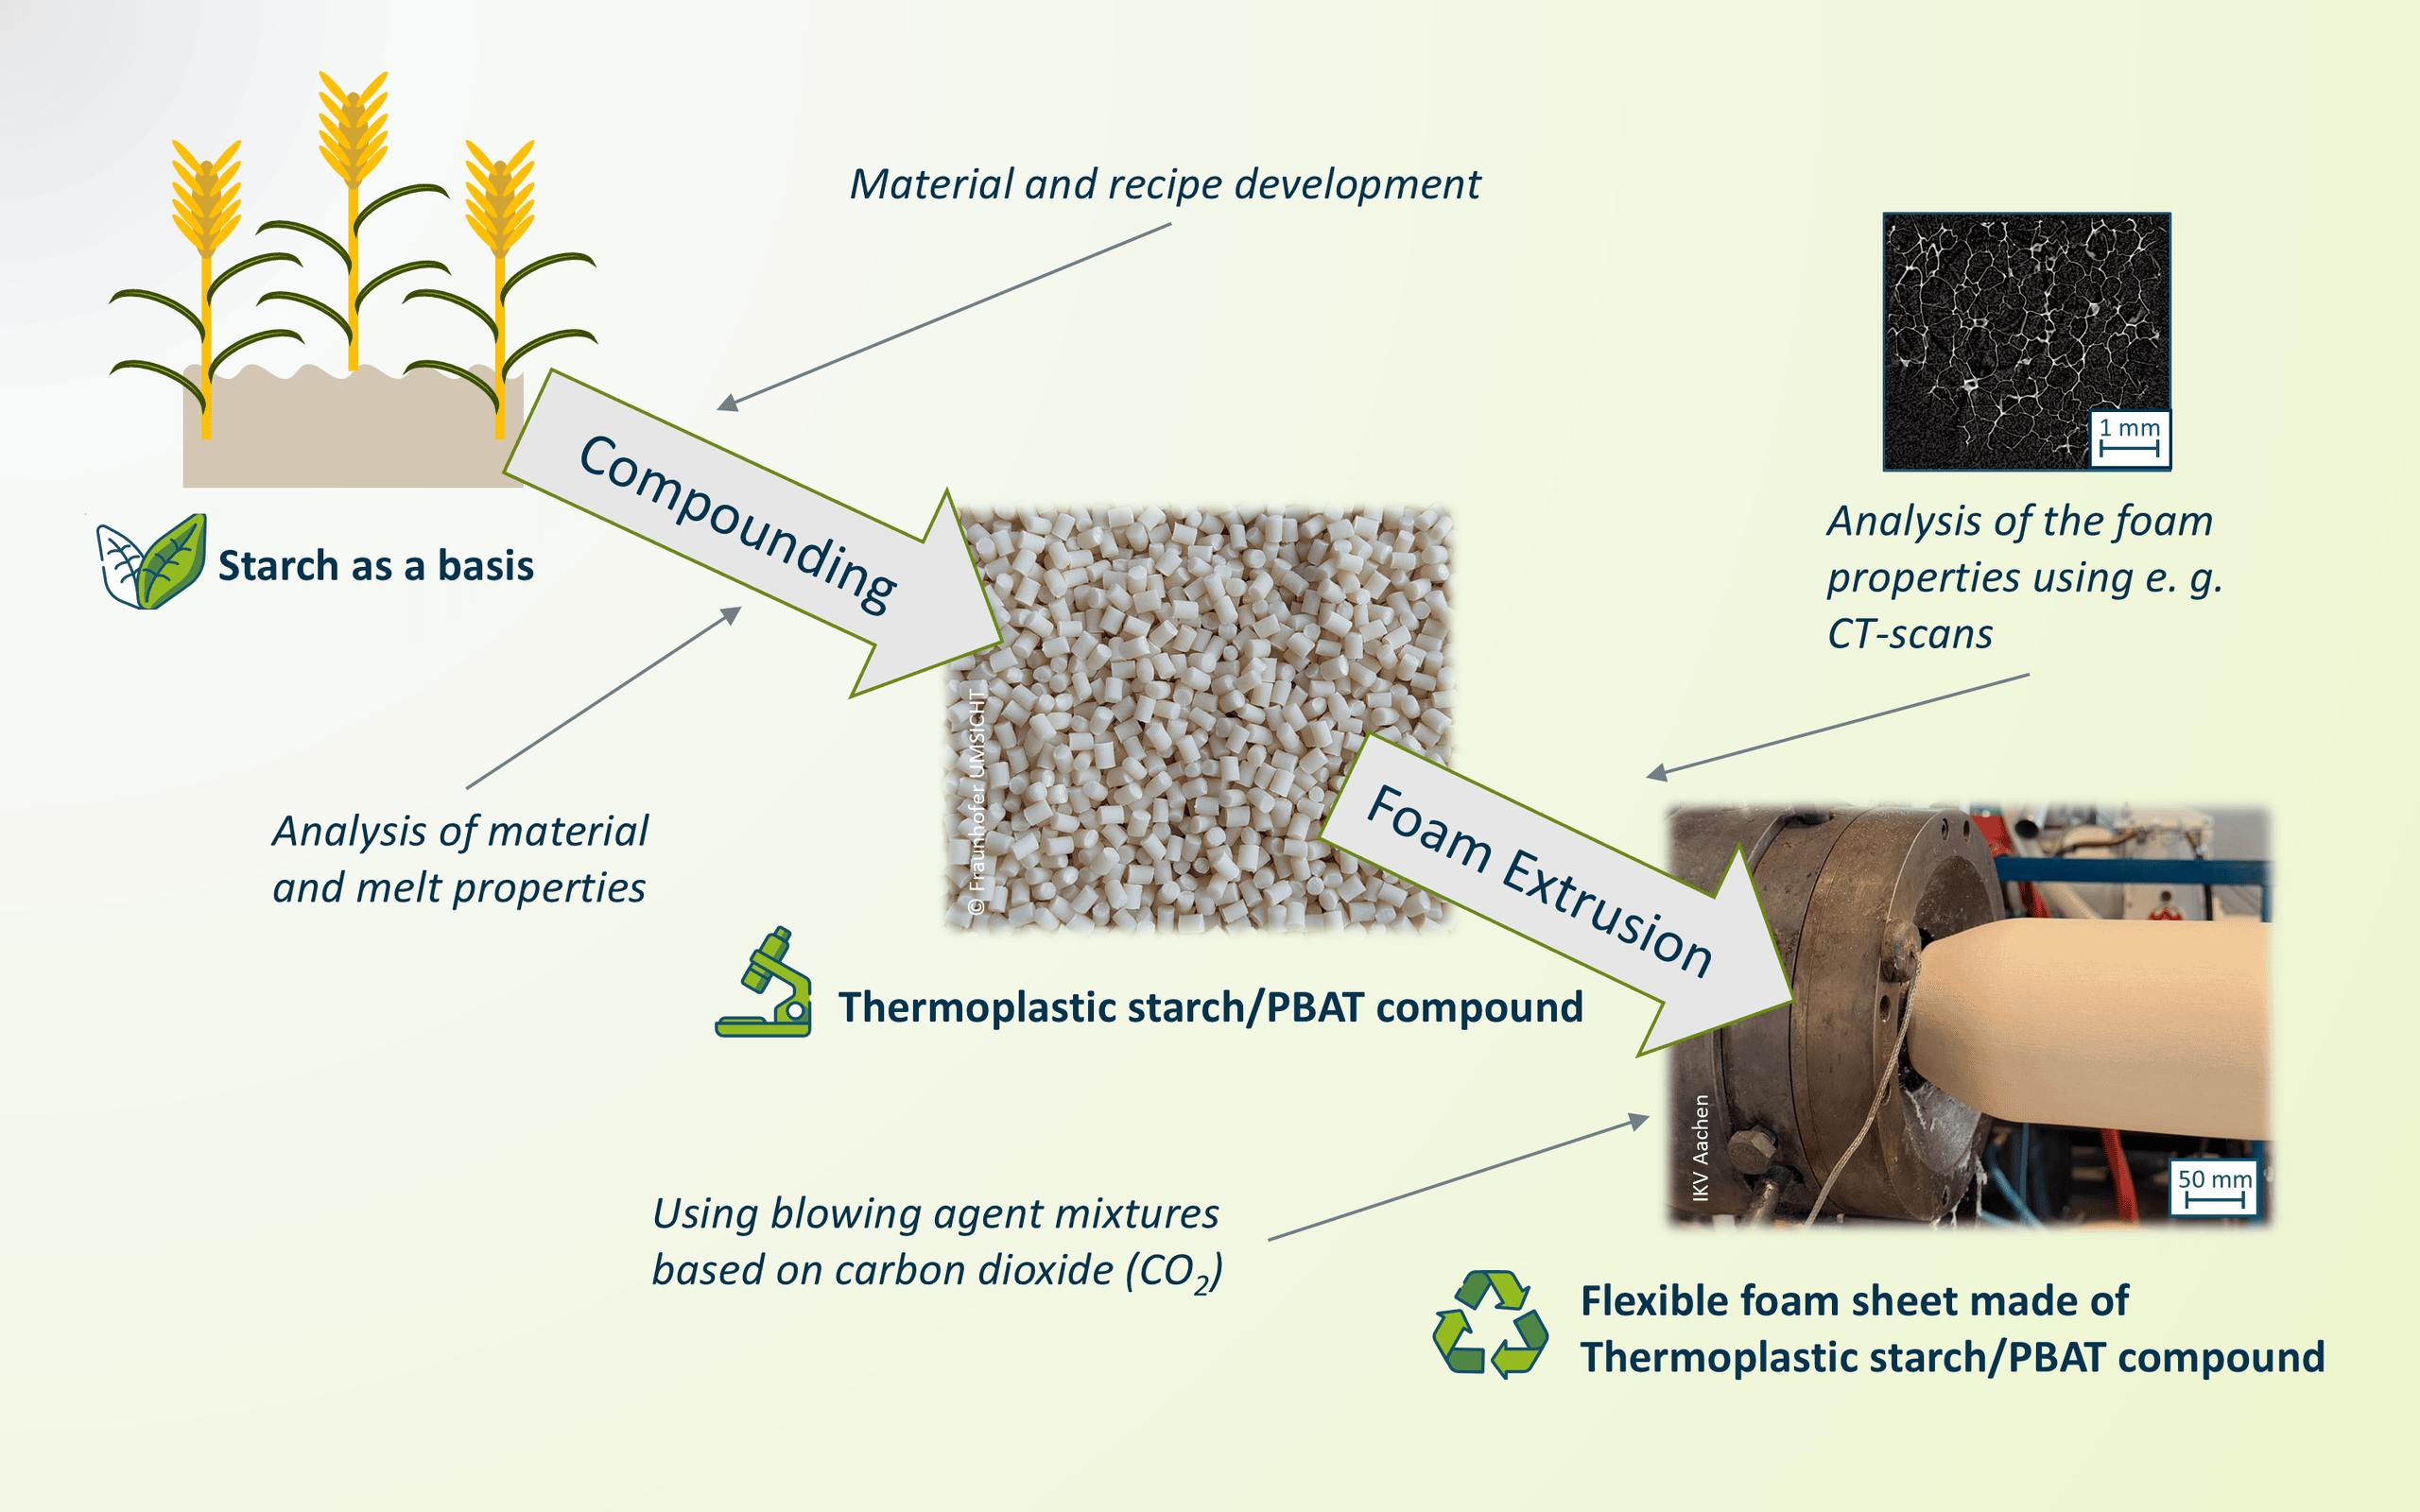
To improve the melt strength and thermomechanical stability of the TPS, blends of plasticized starch and polybutylene adipate terephthalate (PBAT) were first produced during the compounding step by the project partner Fraunhofer UMSICHT in Oberhausen. In a second step, these blends were physically foamed using foam extrusion and processed into either foam strands or flat foam films, whose foam structure was then analyzed (Figure 1).
Figure 1: Starch can be used as a renewable raw material for the production of flexible foam films.
(Source: IKV)
For foaming with CO2, the influence of process parameters such as nozzle temperature and blowing agent content on the expansion ratio, foam density, and cell size was investigated. The foaming tests showed that, with a blowing agent content of 2 wt.% and a mold temperature set to 100 °C, an expansion ratio of approximately 3.86 and a foam density of 0.34 kg/m³ could be achieved. The cells had an average cell diameter of approximately 0.6 mm. A further reduction in the mold temperature to increase the pressure drop and further lower the foam density is not possible, despite a higher blowing agent content, because initial freezing occurs at the nozzle when nozzle temperatures fall below 100 °C.
To conduct the foam film tests, a blowing agent mixture based on CO2 and ethanol was then used. The use of ethanol as a co-blowing agent allows for an expansion of the processing window, as the co-blowing agent increases the solubility of the primary blowing agent, CO2, within the plastic melt. This enables processing at lower process temperatures (nozzle temperature of 95 °C) and the achievement of lower foam densities. Using 2.6 wt% CO2 and 1.1 wt% ethanol, a flexible foam film with a foam density of 0.12 g/cm³ and an average cell diameter of 0.24 mm was produced.
Using thermoplastic starch as a base and physical blowing agents, researchers successfully produced a flexible foam film that can be used industrially, for example, as a more sustainable foam packaging film.
The work was carried out as part of Project 2220NR291C by the Federal Ministry of Food, Agriculture, and Home Affairs (BMELH).
Injection molding of high-performance molded parts with bionic reinforcement inserts
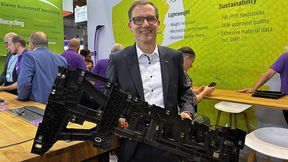
Load-case-optimized integration of fiber reinforcements made from unidirectional (UD) tapes enables the injection molding of high-performance components. As part of the “Lightweight Construction” technology transfer program funded by the Federal Ministry for Economic Affairs and Energy (BMWE), researchers at the IKV demonstrated that the environmental footprint and costs of high-performance components can be reduced even with minimal use of UD tapes. Through targeted reinforcement, the properties of components could be maintained while simultaneously reducing weight and thus material usage, which allowed for the use of a less high-performance but more cost-effective and sustainable mass-produced material.
The research project addressed various challenges associated with this lightweight construction strategy. Since no reliable analysis and evaluation methods for the environmental and economic sustainability of such multimaterial components were available until now, a digital tool was developed as part of the project to analyze and evaluate injection-molded components in terms of their potential for cost savings. The results showed that large, trough-like components—such as storage compartments in vehicles—in particular offer significant potential in this regard.
Date: 08.12.2025
Naturally, we always handle your personal data responsibly. Any personal data we receive from you is processed in accordance with applicable data protection legislation. For detailed information please see our privacy policy.
Consent to the use of data for promotional purposes
I hereby consent to Vogel Communications Group GmbH & Co. KG, Max-Planck-Str. 7-9, 97082 Würzburg including any affiliated companies according to §§ 15 et seq. AktG (hereafter: Vogel Communications Group) using my e-mail address to send editorial newsletters. A list of all affiliated companies can be found here
Newsletter content may include all products and services of any companies mentioned above, including for example specialist journals and books, events and fairs as well as event-related products and services, print and digital media offers and services such as additional (editorial) newsletters, raffles, lead campaigns, market research both online and offline, specialist webportals and e-learning offers. In case my personal telephone number has also been collected, it may be used for offers of aforementioned products, for services of the companies mentioned above, and market research purposes.
Additionally, my consent also includes the processing of my email address and telephone number for data matching for marketing purposes with select advertising partners such as LinkedIn, Google, and Meta. For this, Vogel Communications Group may transmit said data in hashed form to the advertising partners who then use said data to determine whether I am also a member of the mentioned advertising partner portals. Vogel Communications Group uses this feature for the purposes of re-targeting (up-selling, cross-selling, and customer loyalty), generating so-called look-alike audiences for acquisition of new customers, and as basis for exclusion for on-going advertising campaigns. Further information can be found in section “data matching for marketing purposes”.
In case I access protected data on Internet portals of Vogel Communications Group including any affiliated companies according to §§ 15 et seq. AktG, I need to provide further data in order to register for the access to such content. In return for this free access to editorial content, my data may be used in accordance with this consent for the purposes stated here. This does not apply to data matching for marketing purposes.
Right of revocation
I understand that I can revoke my consent at will. My revocation does not change the lawfulness of data processing that was conducted based on my consent leading up to my revocation. One option to declare my revocation is to use the contact form found at https://contact.vogel.de. In case I no longer wish to receive certain newsletters, I have subscribed to, I can also click on the unsubscribe link included at the end of a newsletter. Further information regarding my right of revocation and the implementation of it as well as the consequences of my revocation can be found in the data protection declaration, section editorial newsletter.
Using specifically developed testing methods and a custom-designed test specimen mold, the interaction between the injection-molded component and the reinforcing inserts during the injection molding process was analyzed, and the resulting properties of the finished components were examined. Furthermore, the manufacturing parameters and factors influencing tape quality were investigated using the modified equipment for UD tape production. In addition, an automated optimization routine was developed that determines the load-case-specific placement of UD tape structures within a component, thereby enabling the redesign of existing components to integrate UD tape structures. The project consortium, with the participation of industry partners, successfully produced various reinforced components.
The project was funded as part of the Technology Transfer Program Lightweight Construction by the Federal Ministry for Economic Affairs and Energy (BMWE).
Production Assistance System for Viscosity Control in the Compounding Process
Shear viscosity has a decisive influence on the processability and part quality of plastics. To avoid the negative consequences of fluctuating material viscosity, it is essential to ensure during the compounding process that the shear viscosity meets the target specifications and that fluctuations are minimized.
As part of an IGF project, the IKV utilized a suitable compounding infrastructure to develop a soft sensor for the inline prediction of material viscosity curves of recycled compounds based on comprehensive production data collection, incorporating all necessary peripheral devices and process equipment. This soft sensor forms the basis for an assistance system that predicts the viscosity of plastic melts inline during the compounding process and, based on this, suggests appropriate formulation adjustments to achieve a target viscosity that is as constant as possible.
To develop such a soft sensor, a sufficiently large database first had to be established. To this end, a three-stage slit rheometer was used, which was calibrated based on individual shear viscosity curves measured in the laboratory for characteristic shear rates. This rheometer was then used to generate the data necessary for developing AI models. To specifically influence the material’s viscosity, various types of polypropylene—including virgin material and recycled material—as well as peroxide masterbatches were used to modify the viscosity as needed.
For inline prediction, a soft sensor in the form of a neural network was developed that predicts the viscosity curve based on the parameters of rotational speed, pressure, temperature, and torque. In addition, a formulation-based model was developed that describes the influence of material composition on viscosity using established mixing rules. The database includes 120 polypropylene compounds with varying polymer and PCR types (MFR 3.5–47 g/10 min), as well as different peroxide contents.
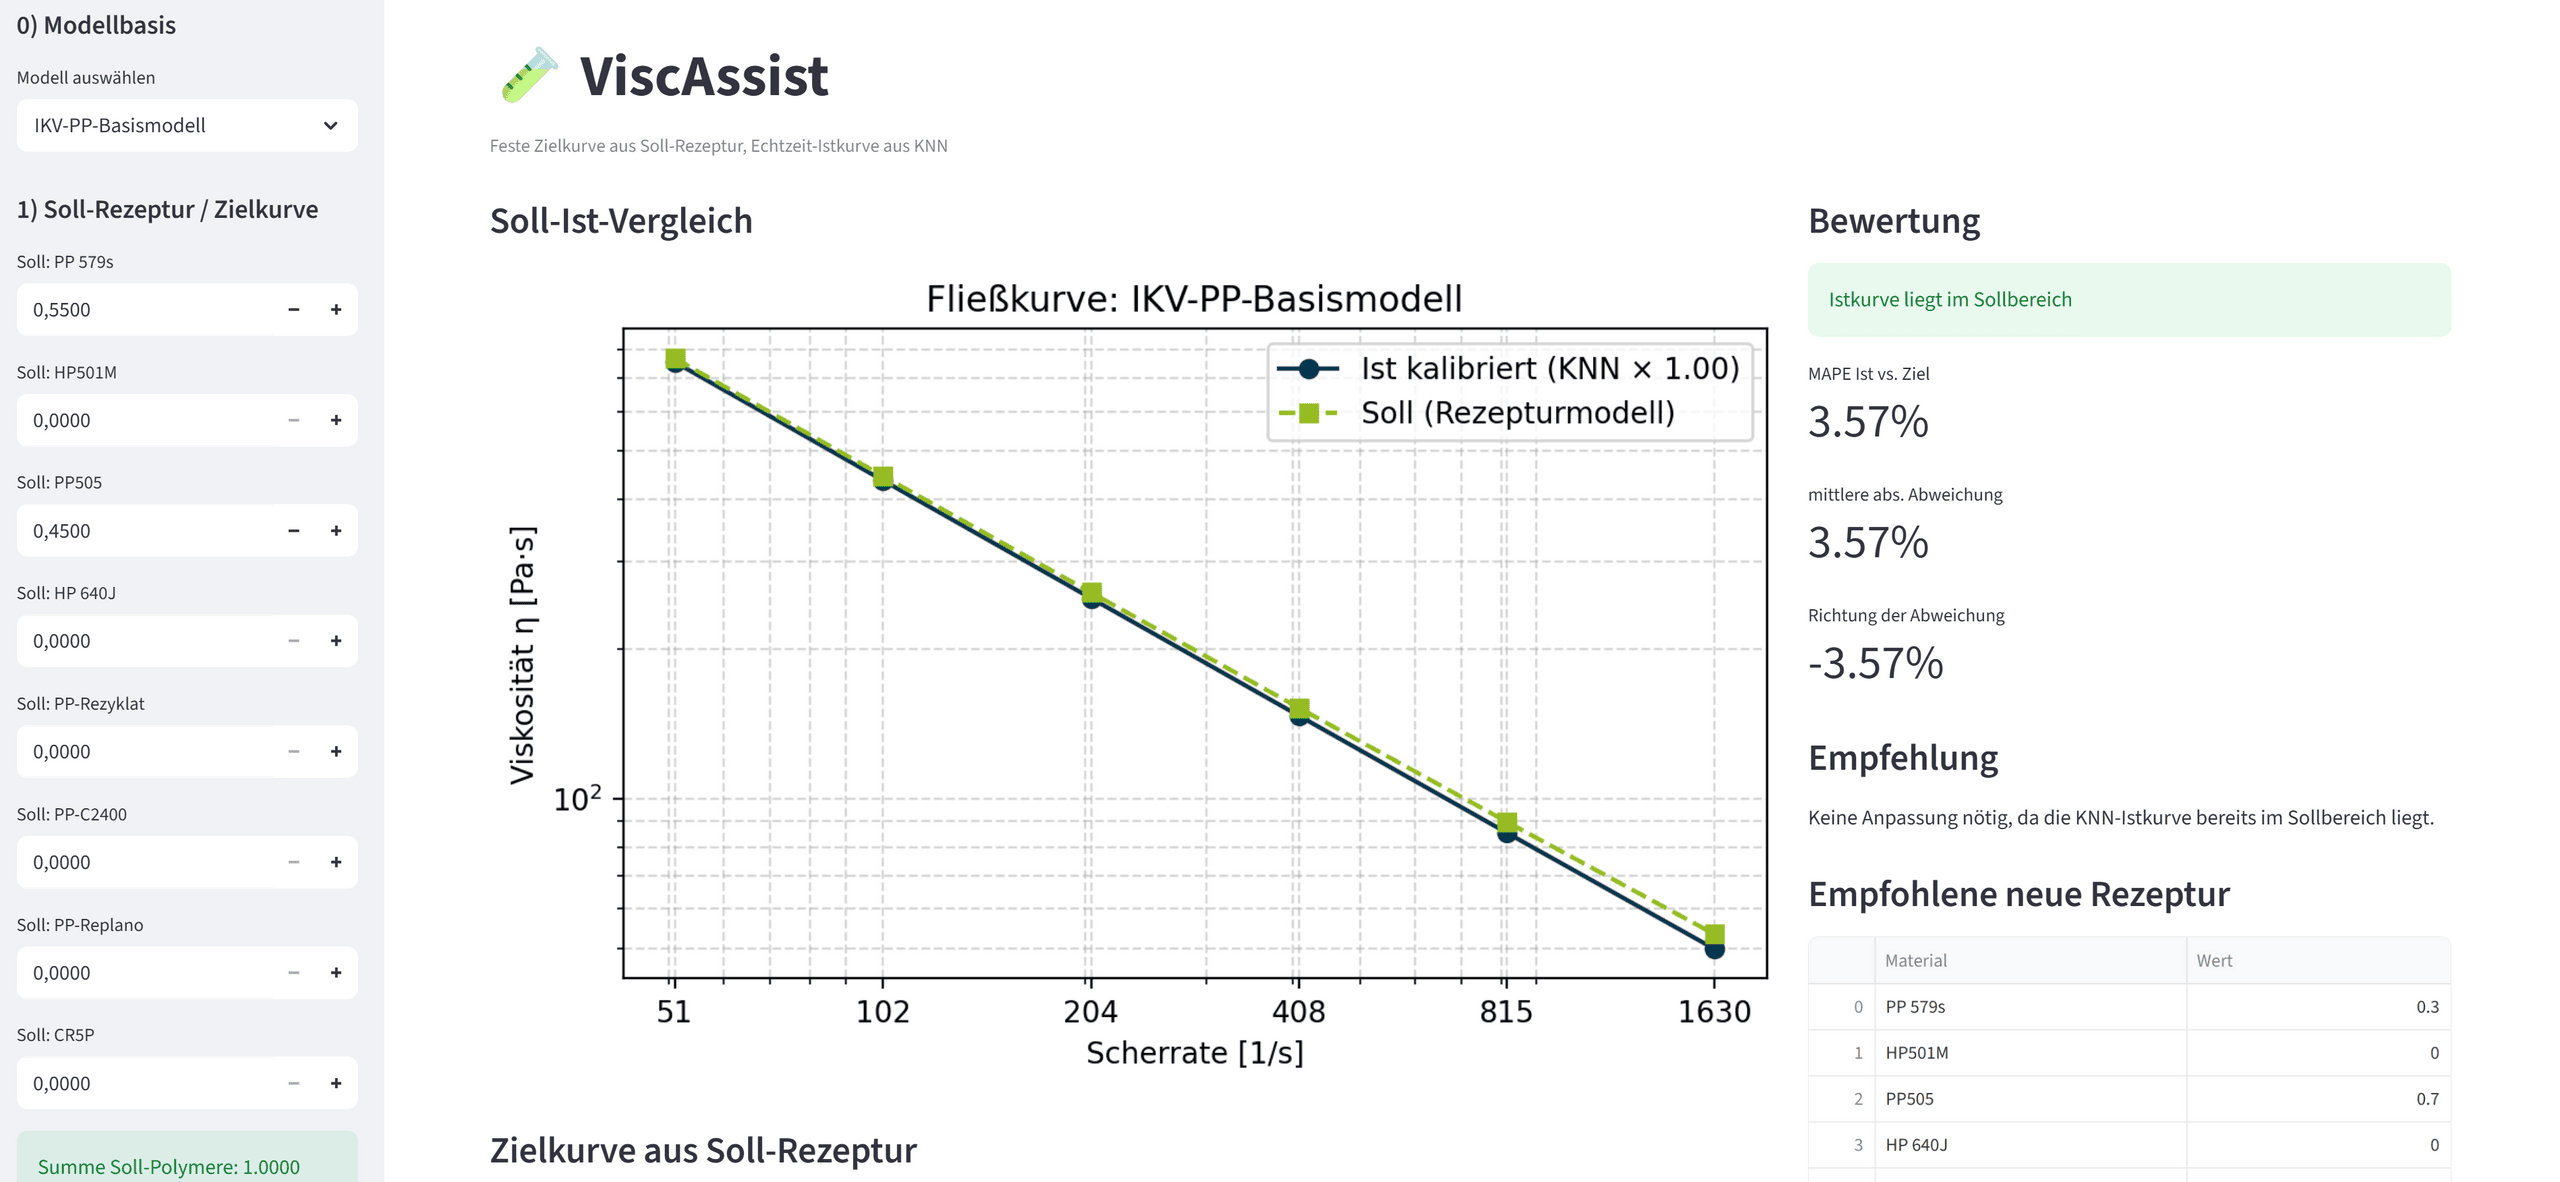
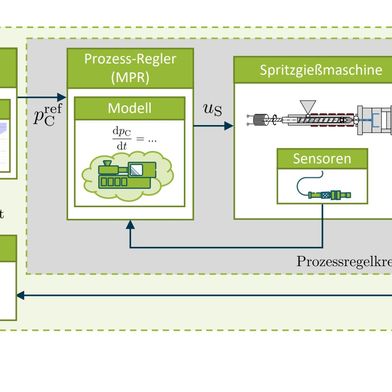
By combining both models, the soft sensor can be used to determine a current actual viscosity curve from process data and compare it with a target curve calculated from the mixing rules. Based on this, a recommendation model is used to derive targeted adjustments to the material proportions in order to approximate the target curve (Figure 2). The actual viscosity can be predicted for known formulations with an R² of 0.92, while the formulation model achieves a model quality of R² = 0.98. Viscosity can be predicted with deviations of 10%. For a fully functional assistance system, viscosity prediction still needs to be optimized; however, the system is already capable of reliably detecting viscosity fluctuations in the compound and providing recommendations for adjusting the formulation. This results in more homogeneous material properties for the subsequent process. This leads to more efficient and sustainable production that meets current industry requirements.
Figure 2: The soft sensor developed at the IKV enables the inline prediction of material viscosity curves for recycled compounds. In combination with a formulation-based model, the assistance system can use this data to derive formulation recommendations.
(Source: IKV)
This work is supported by the Federal Ministry for Economic Affairs and Energy (BMWE) as part of IGF Project 23179 N.
Prof. Dr.-Ing. Christian Hopmann IKV-Institutsleitung und Lehrstuhl für Kunststoffverarbeitung