At Fakuma 2026, the companies Boy and Evonik demonstrated the processing of a bioresorbable polymer using microinjection molding. Using an 8-mm plasticizing unit and a micro hot-runner system, two medical microscrews, each weighing 0.065 g, were produced without a sprue. The material residence time was approximately four minutes.
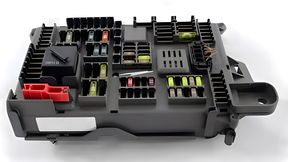
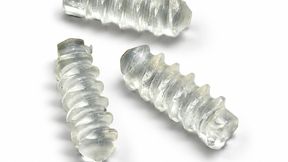
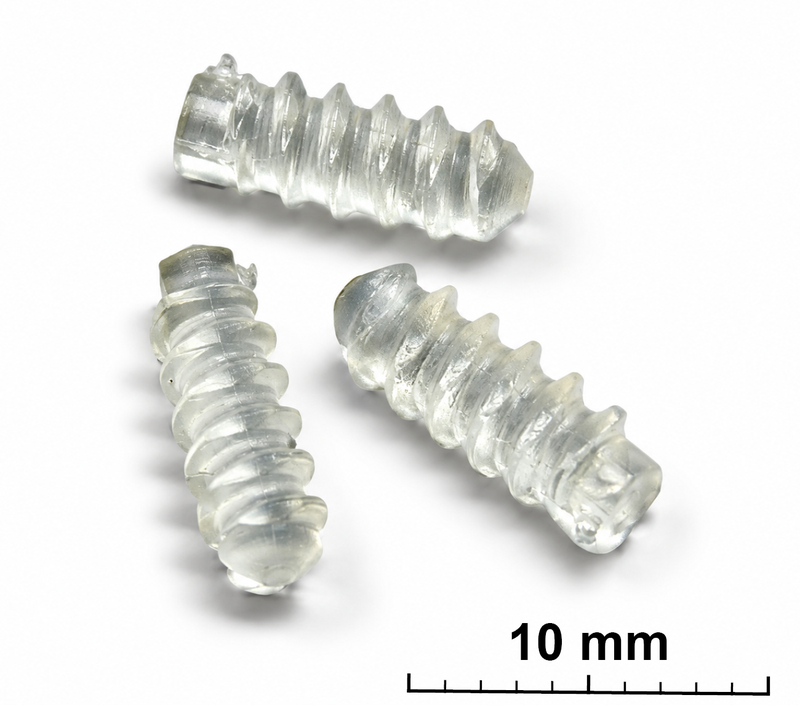
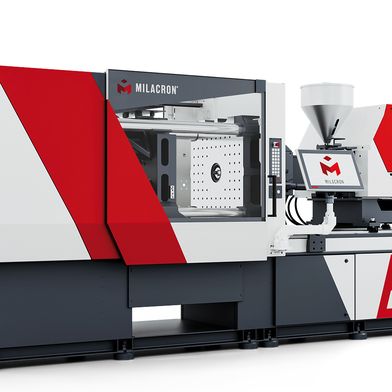
Medical microscrews made from Evonik’s bioresorbable polymer Resomer LR 704 S, manufactured using microinjection molding on a Boy XS E with an 8-mm plasticizing unit and the L2X-Mikro microhot-runner system from Ewikon.
(Bild: Boy)
Today, many medical products are manufactured using micro-injection molding. In addition to the very low part weights, the reproducibility of the process and the dwell time of the plastic in the machine play a particularly crucial role.
In practice, however, standard injection molding machines—which were not originally designed for such small shot weights—are often used to manufacture micro-injection-molded parts. To ensure stable production nonetheless, a large portion of the shot volume is often used for the sprue. This not only makes it more difficult to control the process but also impairs the effectiveness of monitoring and control functions. At the same time, significant material losses occur.
Practical experience shows that, for shot weights of less than one gram, often less than five percent of the material used actually ends up in the molded part. While this approach is often considered economically acceptable for low-cost, standard plastics, it quickly reaches its limits when it comes to high-priced materials where dwell time is critical.
Designed specifically for the lightest shot weights
To meet these requirements, Boy developed an 8-mm micro-injection molding screw. It operates according to the classic three-zone first-in, first-out principle. Pre-metering was deliberately omitted in order to keep the material’s residence time as short as possible and to avoid stagnation zones.
Due to the small screw diameter, the 8-mm unit also offers significantly higher process resolution. Compared to a 14-mm screw, this represents a 3.1-fold improvement. In addition, the backflow preventer closes more quickly due to its design, which further increases the reproducibility of the injection molding process.
Short dwell times thanks to optimized system technology
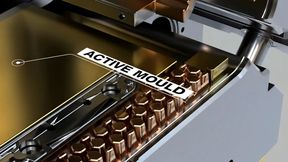
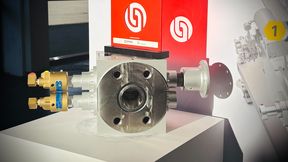
When combined with the L2X-Mikro micro hot-runner system from Ewikon , very short residence times can be achieved thanks to the compact design and low material volumes. This enables gate-free processing of thermally sensitive plastics, such as the bioresorbable and biocompatible polymer Resomer LR 704 S from Evonik Industries AG.
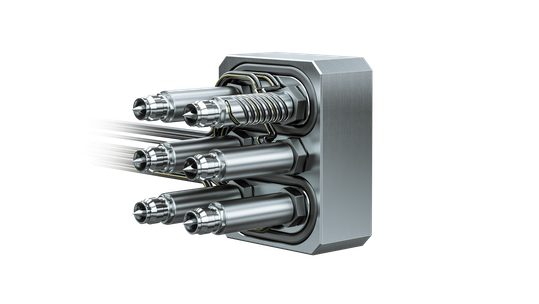
Thanks to its compact design and low material volumes, Ewikon's L2X-Mikro micro hot-runner system enables very short dwell times.
(Bild: Ewikon)
The particular challenge in processing this material lies in the degradation of the polymer chains. Even exceeding the permissible dwell time can lead to undesirable material degradation. Since bioresorbable plastics are associated with high material and regulatory costs, eliminating sprues offers significant cost-saving potential.
Practical Demonstration at Fakuma 2026
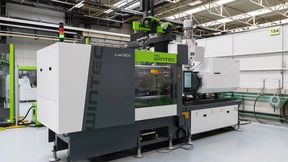
At Fakuma 2026, the concept’s capabilities were demonstrated in a joint application by Boy, Ewikon, and Evonik. At Boy’s booth, a medical microscrew was manufactured on a Boy XS E equipped with an 8-mm plasticizing unit.
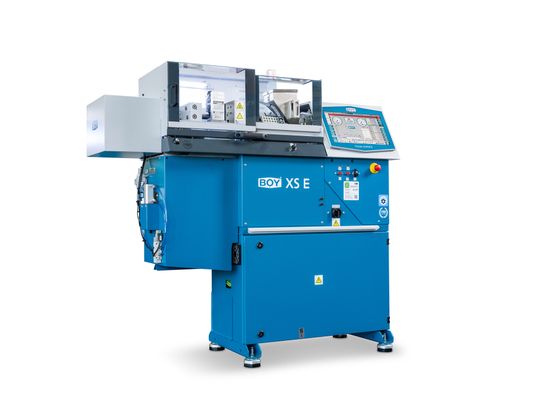
The combination of the Boy XS E's 8-mm plasticizing unit and the L2X micro hot-runner system enables short residence times, high reproducibility, and a significant reduction in material loss.
(Bild: Boy)
The material used was Resomer LR 704 S. Two micro screws, each weighing 0.065 g, were injection-molded directly into the part. The total shot weight was thus only 0.13 g. With a cycle time of 12 seconds, a total material residence time of approximately four minutes was achieved in the plasticizing unit and hot runner system.
By comparison, the residence time would have been about 11 minutes under identical process parameters and using a 14-mm unit. In that case, a significantly greater degradation of the polymer chains would have been expected. The results of the experiment were confirmed by Evonik’s application engineering team.
Conclusion
The results presented at Fakuma 2026 demonstrate that even high-cost plastics with critical dwell times can be processed economically and reliably in micro-injection molding, provided that the machine and hot-runner technology are consistently designed to meet the requirements of the smallest shot weights. The combination of the Boy XS E’s 8-mm plasticizing unit and the L2X micro hot-runner system enables short residence times, high reproducibility, and a significant reduction in material loss. This opens up new possibilities for cost-effective series production in micro-injection molding, particularly for bioresorbable and medical-grade specialty plastics. (sl)
Date: 08.12.2025
Naturally, we always handle your personal data responsibly. Any personal data we receive from you is processed in accordance with applicable data protection legislation. For detailed information please see our privacy policy.
Consent to the use of data for promotional purposes
I hereby consent to Vogel Communications Group GmbH & Co. KG, Max-Planck-Str. 7-9, 97082 Würzburg including any affiliated companies according to §§ 15 et seq. AktG (hereafter: Vogel Communications Group) using my e-mail address to send editorial newsletters. A list of all affiliated companies can be found here
Newsletter content may include all products and services of any companies mentioned above, including for example specialist journals and books, events and fairs as well as event-related products and services, print and digital media offers and services such as additional (editorial) newsletters, raffles, lead campaigns, market research both online and offline, specialist webportals and e-learning offers. In case my personal telephone number has also been collected, it may be used for offers of aforementioned products, for services of the companies mentioned above, and market research purposes.
Additionally, my consent also includes the processing of my email address and telephone number for data matching for marketing purposes with select advertising partners such as LinkedIn, Google, and Meta. For this, Vogel Communications Group may transmit said data in hashed form to the advertising partners who then use said data to determine whether I am also a member of the mentioned advertising partner portals. Vogel Communications Group uses this feature for the purposes of re-targeting (up-selling, cross-selling, and customer loyalty), generating so-called look-alike audiences for acquisition of new customers, and as basis for exclusion for on-going advertising campaigns. Further information can be found in section “data matching for marketing purposes”.
In case I access protected data on Internet portals of Vogel Communications Group including any affiliated companies according to §§ 15 et seq. AktG, I need to provide further data in order to register for the access to such content. In return for this free access to editorial content, my data may be used in accordance with this consent for the purposes stated here. This does not apply to data matching for marketing purposes.
Right of revocation
I understand that I can revoke my consent at will. My revocation does not change the lawfulness of data processing that was conducted based on my consent leading up to my revocation. One option to declare my revocation is to use the contact form found at https://contact.vogel.de. In case I no longer wish to receive certain newsletters, I have subscribed to, I can also click on the unsubscribe link included at the end of a newsletter. Further information regarding my right of revocation and the implementation of it as well as the consequences of my revocation can be found in the data protection declaration, section editorial newsletter.